01 / CUSTOMER PROBLEM
Control heat and geometry
A prepreg tool must hold its surface and size through cure and later thermal cycles. A defined cure route reduces guesswork around consolidation, spring-back, voids and dimensional drift.
 TOOLING MATERIALS
Product family
EPTEK tooling prepregs are limited to LTP220 and LTP240. LTP220 and LTP240 are presented with their cure routes and source-verified service-temperature information.
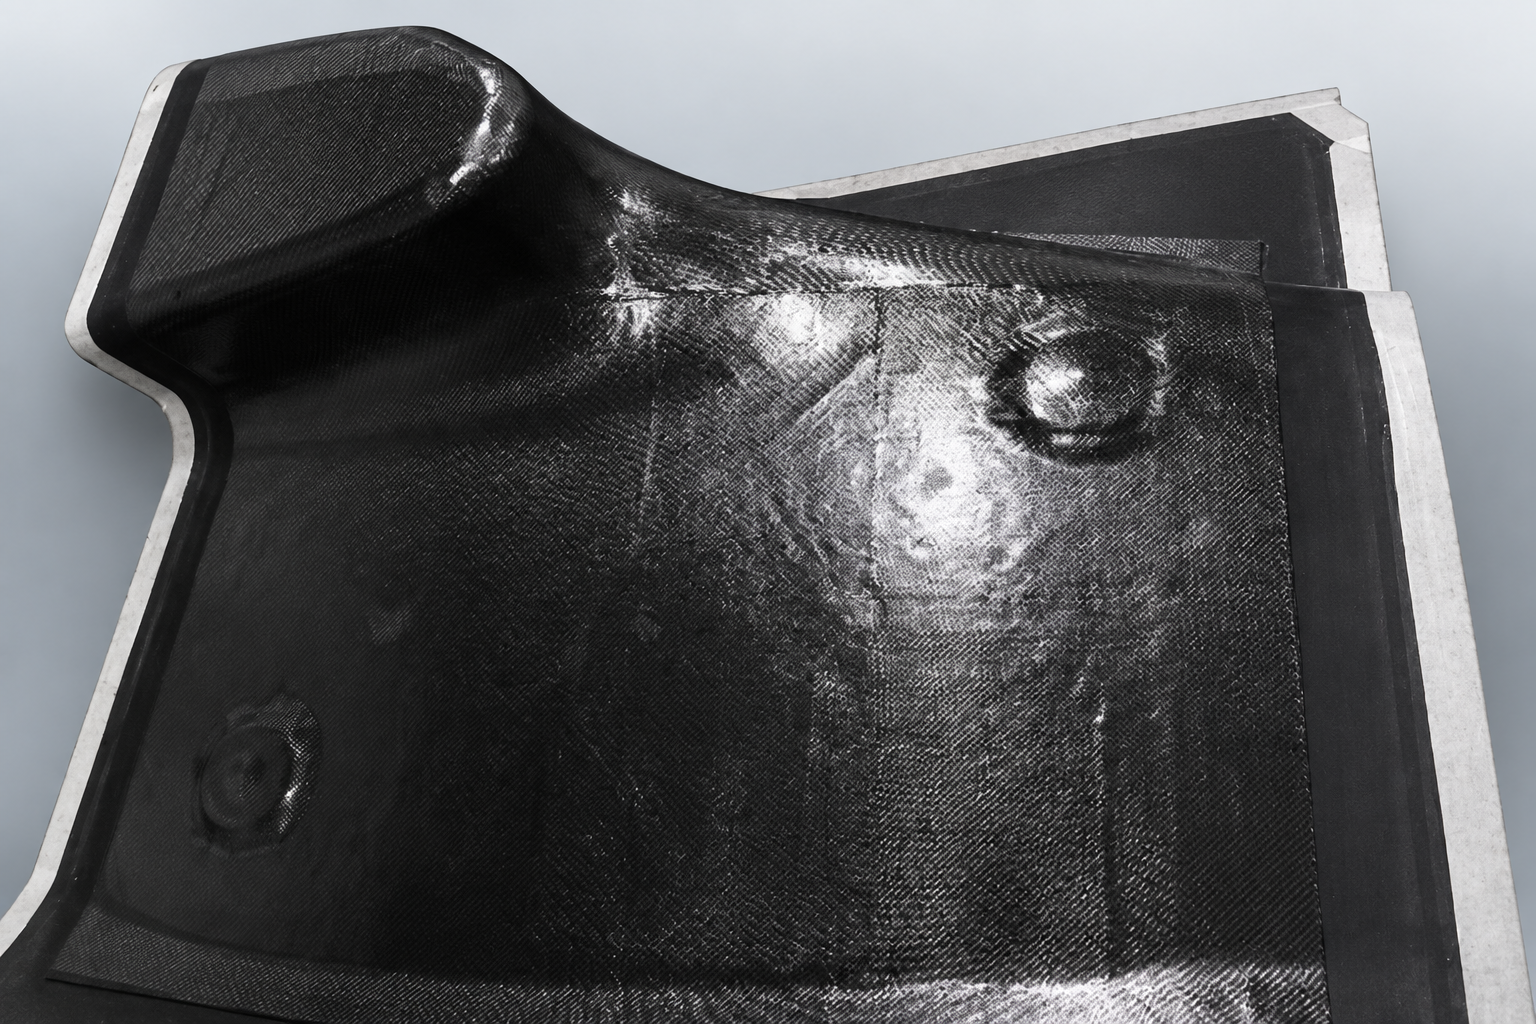
Engineering view / Tooling prepregs
Prepreg tooling is a controlled system: resin, reinforcement, storage, lay-up, vacuum or pressure and cure work together. EPTEK’s tooling prepreg routes distinguish practical low-temperature initial cure from higher-temperature curing for more demanding composite tools.
01 / CUSTOMER PROBLEM
A prepreg tool must hold its surface and size through cure and later thermal cycles. A defined cure route reduces guesswork around consolidation, spring-back, voids and dimensional drift.
02 / SELECTION LOGIC
Use LTP220 and LTP240 according to the project’s cure temperature, thermal exposure, tooling size, pressure route and inspection requirement. Do not transfer a Tg or service claim from one grade to another.
03 / PROCESS CHECKPOINTS
Record storage, conditioning, lay-up, debulk, vacuum integrity, bagging, cure, post-cure, trim and surface inspection. Keep the actual laminate thickness and cure history with the tool record.
04 / RELEASE CHECK
Prepreg, gelcoat or surface film, backing structure, release system and repair method should be trialed together. The linked TDS remains the authority for cure and handling limits.
Product data
The tooling prepreg family is intentionally limited to the two published routes below.
01 / LTP220
Low-temperature tooling prepreg
02 / LTP240
High-temperature tooling prepreg
01 / PRODUCT FAMILY
Low-temperature pre-cure tooling route; confirm cure and service limits in the TDS.
02 / PRODUCT FAMILY
LTP240 is the high-temperature-curing tooling-prepreg version; cure and DMA reference data are defined in its technical data sheet.