01 / GEOMETRY
Design for moulding and withdrawal
Set draft, fillets, parting and machining allowances with the foundry. Locate core prints and assembly datums so the pattern supports the intended core position in the sand mould.
 TOOLING MATERIALS
Application / Foundry
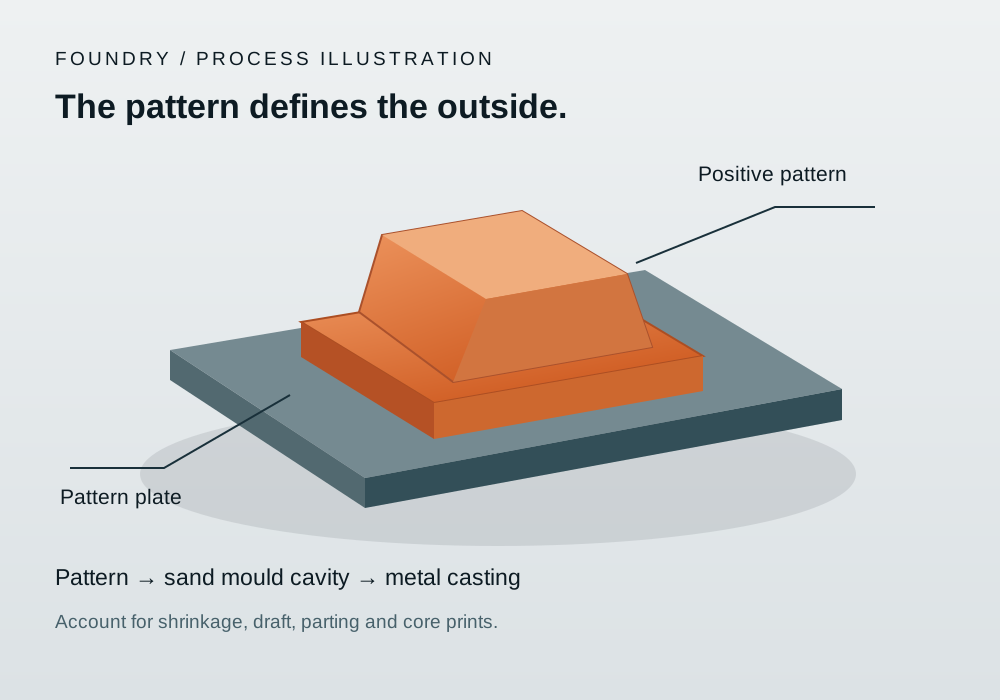
A foundry pattern creates the external cavity in a sand mould. Pattern geometry includes the casting allowance, draft, parting arrangement and core prints. Reusable resin and board tooling must preserve that geometry while resisting the wear of repeated sand contact.
Engineering requirements
01 / GEOMETRY
Set draft, fillets, parting and machining allowances with the foundry. Locate core prints and assembly datums so the pattern supports the intended core position in the sand mould.
02 / PRODUCTION DUTY
Sand type, compaction method, release practice and the number of moulding cycles influence wear. Thin ribs, edges and locating features may need local reinforcement or replaceable details.
Engineering requirements
| Manufacturing need | Material family | Selection focus |
|---|---|---|
| Master or low-duty development pattern | PUBOARD model boards | Ease of machining, surface finish and sealing; distinguish a master from production tooling |
| Machined production pattern and plate | PUBOARD 1250 for patterns; PUBOARD 1350 for Coldbox models and matchplates | Abrasion resistance, edge strength, stability, bonding and repairability |
| Replicated or cast pattern | project-specific PU or epoxy casting systems, subject to foundry-process qualification | Casting section, filled-system behaviour, cure, hardness and tested sand-wear performance |
| Surface and repair system | Selected gelcoats and compatible repair materials | Adhesion, wear, detail reproduction and compatibility with the underlying material |
Choose the exact grade against the foundry process and trial wear results. Density or hardness alone is not a substitute for abrasion performance in the actual sand system.
Engineering requirements
Confirm dimensions after cure and machining, then verify the first sand mould and trial casting. Plan how worn edges, core prints and damaged surfaces will be repaired without moving the reference geometry.