Aerospace tooling
Choosing Casting Resins for Aerospace Stretch-Forming Moulds
The right casting resin depends first on how the working face will be created. A blank that will be CNC-machined has a different risk profile from an upper tool copied directly against a finished lower tool.
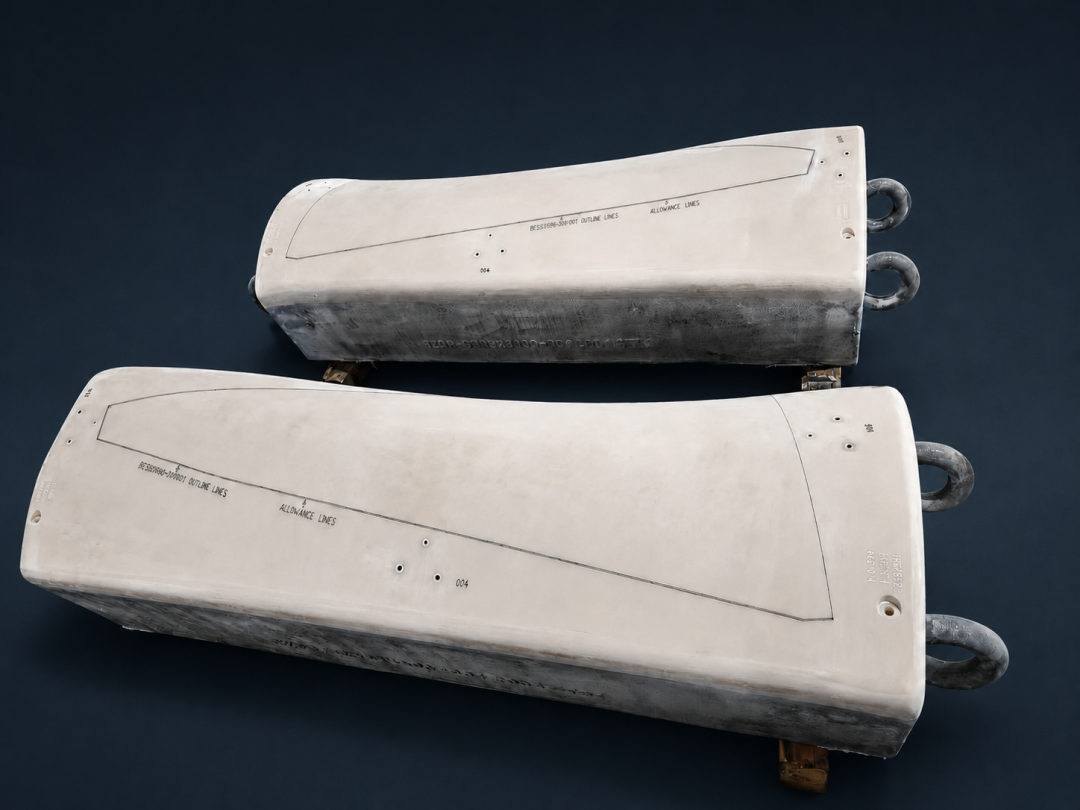
Aerospace stretch-forming, straightening and sizing moulds combine large envelopes, compound curvature and repeated loading. The mould body must tolerate pressure and local impact while remaining machinable and dimensionally stable through cure, machining and use. In practice, the decisive question is not simply which resin has the higher headline property. It is whether the cast surface will be removed by CNC or retained as the finished working face.
Two routes create two different material jobs
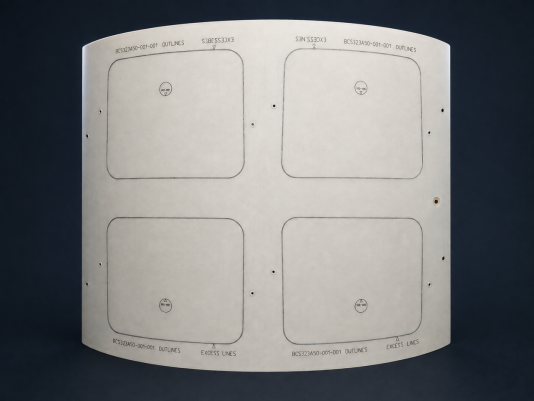
Most projects cast a near-net blank, allow it to cure and stabilise, then machine the working face, perimeter, datum features and holes. In that route, the casting surface is sacrificial. The process therefore prioritises thick-section integrity, manageable exotherm, toughness, machinability and predictable dimensional change.
A paired tool can follow a different route. The lower tool is machined to final geometry, then a controlled gap layer—such as precision wax, or a suitable metal shim—represents the sheet thickness and process clearance. The upper tool is cast against that interface. After demoulding, its back and mounting features may be machined, but the working face is left as cast. Any pinhole, trapped air pocket, wrinkle or local lack of fill at the interface can therefore remain in the finished tool.
What PUCAST 260 is suited to
PUCAST 260 is a two-component polyurethane casting resin that can be used with fillers. The reference data lists an unfilled mixed viscosity of about 850 mPa·s at 25°C, which supports filling complex cavities and transitions; filler choice can then tune density and stiffness. The same table lists Shore D 85, a typical flexural modulus of about 4,300 MPa, compressive strength of about 85 MPa and typical linear shrinkage of about 0.1%.
For thick blanks, the reference table lists a maximum cast thickness of 400 mm*. That figure is a process boundary to validate, not a permission to pour any geometry at that thickness. Total mass, cavity shape, resin and filler temperature, ambient temperature and heat release must be checked for each pour. Where the blank will be machined, PUCAST 260 is the natural candidate when a large section, casting efficiency and subsequent cutting performance carry the most weight.
Moisture control is central. Isocyanate chemistry can react with water and generate carbon-dioxide microbubbles. Dry raw materials and fillers, a controlled room, dry tools and moulds, short open-container time, low-position feeding and mixing that limits entrained air are part of the process window. They cannot be replaced by a late-stage cosmetic fix if bubbles will be exposed by machining.
What EPCAST 75 is suited to
EPCAST 75 is a pre-filled, two-component epoxy system mixed at 100:15 by weight. The reference data gives a mixed viscosity of 3,000–5,000 mPa·s at 25°C and a typical working time of 100–120 minutes for a 500 g mix at 25°C. That longer, explicitly tested window helps when a large interface has a long feed path, several high-point vents or a sequence of continuous wetting operations.
The grade is also suited to direct upper-tool replication because epoxy does not have the same isocyanate–water gas reaction. The reference values list Shore D 85, tensile strength 40–60 MPa, flexural strength 60–75 MPa, compressive strength above 80 MPa and a typical linear CTE of about 50 × 10−6 K−1. A single buildup is recommended up to 80 mm*. Thicker bodies need a designed, validated layered or zoned structure with controlled interlayer timing, heat release and cooling.
Process controls decide whether the numbers matter
For direct replication, first confirm the lower-tool geometry, gap thickness and edge seal. On a direct-copy job, resin should wet the working face continuously before the backing volume is filled. Feed points belong at low areas and vents at geometric high points; a closed air pocket becomes a surface defect. Choose a wax or metal gap layer that meets the required thickness, conformity and release conditions.
Post-cure and cooling belong in the machining and acceptance plan. A useful sequence is rough machining, stabilisation and reinspection, then semi-finish and finish machining. For EPCAST 75, the stated strength and CTE values are typical technical-data-sheet results, not design allowables. For PUCAST 260, the same applies to viscosity, modulus, compressive strength and thickness. Confirm the actual batch, mix, temperature, geometry and equipment before setting an allowable.
Selection in one decision
| Decision point | PUCAST 260 | EPCAST 75 |
|---|---|---|
| Primary route | Large, thick near-net blank followed by CNC | Direct upper-face replication; also precision blanks |
| Reference mixed viscosity | About 850 mPa·s at 25°C, unfilled | 3,000–5,000 mPa·s at 25°C |
| Reference working time | About 50 min, 500 g at 20°C | 100–120 min, 500 g at 25°C |
| Thickness reference | Maximum cast thickness 400 mm* | Recommended single buildup 80 mm* |
| Main controls | Dryness, mixing air, filler and thick-section exotherm | Interface wetting, high-point venting, layer timing and post-cure |
*Values above are typical reference data. They are not design allowables or universal guarantees; validate the proposed mix, section and cure schedule with a sample or first article. If the final face will be machined, start by sizing the blank and controlling heat. If it will not be machined, start by protecting the interface and the air-escape path; that is why EPCAST 75 is generally the stronger starting point for direct replication.