Application / Foundry

Core Boxes and Sand-Core Tooling

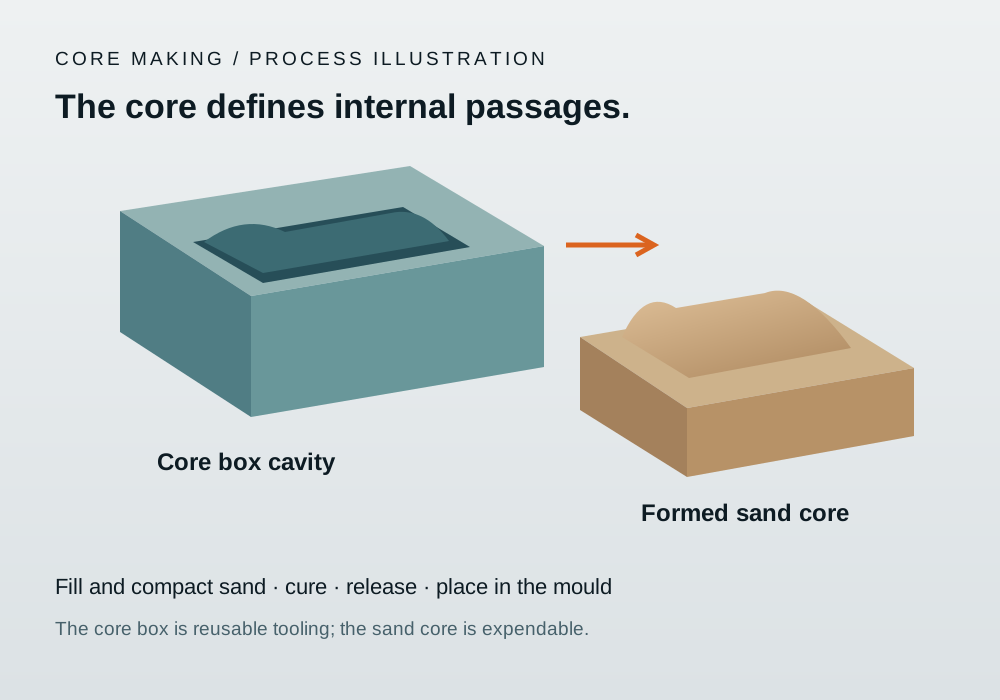
A core box forms the expendable sand core that creates an internal cavity in a metal casting. The reusable core box needs accurate joints, repeatable location, adequate venting and reliable core release. Its duty differs from an external foundry pattern.

Original schematic showing a reusable core box and a formed sand core
EPTEK / APPLICATIONReusable core box, expendable sand core

Engineering requirements

Design around the core-making method

01 / PROCESS

Cold-setting and heated processes need different tools

Specify the sand and binder, filling or shooting method, curing process and actual tool temperature. A resin board or cast resin suitable for one process is not automatically suitable for a heated core box.

02 / TOOL DESIGN

Protect the features that control the core

Plan parting, vents, filling points, ejection, locating bushes and replaceable wear areas. Joints must remain aligned and sealed during repeated filling and demoulding.

Engineering requirements

Select the body and working surface

RouteEPTEK familyProject check
CNC-machined core boxPUBOARD 1350 for Coldbox core boxesSand abrasion, detail strength, joints, inserts and operating temperature
Cast or replicated core boxproject-specific casting systems, subject to core-making trialsRelease behaviour, fillers, cure, dimensional change and wall thickness
Surface layer or repairCompatible tooling gelcoats and repair systemsAdhesion, edge detail, abrasion and repair machining

Engineering requirements

Verify the core before production

Trial the actual sand and binder system. Inspect core dimensions, parting-line mismatch, surface damage and release consistency. Follow with a casting trial to confirm core location and the resulting internal geometry.