01 / CORE MATERIAL
Balance weight and compression
Select the PUFOAM grade against the required density, compressive behaviour, closed-cell structure and water exposure. The core, surrounding shell and load paths must be assessed together.
 TOOLING MATERIALS
Application / Wind energy
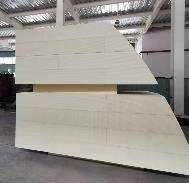
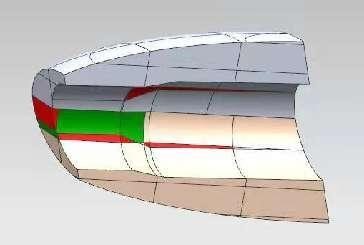
PUFOAM core blocks for floating offshore wind pontoons are manufactured, bonded and machined as a coordinated assembly. Block layout, bond quality and final geometry determine how reliably the core fits the surrounding structure.
Engineering requirements
01 / CORE MATERIAL
Select the PUFOAM grade against the required density, compressive behaviour, closed-cell structure and water exposure. The core, surrounding shell and load paths must be assessed together.
02 / MANUFACTURING
Divide the CAD model into blocks that can be bonded, fixtured, machined and transported. Retain common reference points between the bonding platform, CNC fixture and final assembly.
Engineering requirements
| Stage | What must be controlled |
|---|---|
| Bonding | Clean and prepare the foam faces; control adhesive coverage, joint gaps, positioning and clamping throughout cure. |
| Machining | Maintain common datums; machine mating faces, outer contours and designed bond-flow grooves without damaging the foam. |
| Inspection and delivery | Check contour and joint fit; identify each block against the assembly drawing, remove dust and protect surfaces against moisture and transport damage. |
| Assembly validation | Confirm the chosen foam and adhesive together under the project load and water-exposure conditions. |